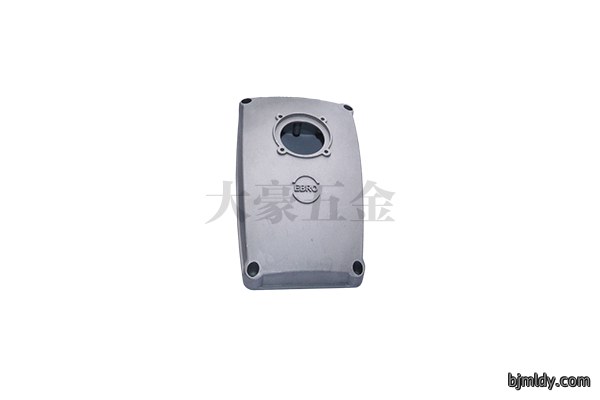
The design of die casting must take into account seven critical aspects that collectively ensure both manufacturability and functional performance throughout the production process. The first consideration involves wall thickness of die casting, which directly impacts metal flow, cooling rates, and the structural integrity of the final component.
Casting round corner design specification represents a fundamental principle in the die casting industry that addresses multiple critical manufacturing and finishing requirements across the production lifecycle. Within the domain of metal die casting processes, each structural component of a die casting mold should incorporate rounded corners at all intersection points between surfaces, with the notable exception of parting surfaces where dimensional precision takes precedence over radial transitions. This design approach serves several interconnected functional purposes that directly impact casting quality and downstream processing efficiency.
Design specifications for inserts in die casting parts constitute a critical dimension of the manufacturing engineering discipline, requiring careful attention to multiple integrated parameters that collectively determine component functionality and service longevity. First, the quantity of inserts embedded within die casting parts demands judicious constraint; excessive insert placement introduces unnecessary complexity into the casting process while simultaneously amplifying production costs and reducing overall structural integrity of the final component. The optimization of insert count directly influences mold design feasibility and casting cycle efficiency within the manufacturing workflow.
During the metal casting manufacturing process, a defect condition can occur where porti
Causes :1, die casting mold temperature is too low; 2, the liquid metal temperature is low; 3, the press pressure is too small, 4, the metal liquid is insufficient, the injection speed is too high; 5, the air can not be discharged.
Adjustment method :1, 2, increase the die casting mold, liquid metal temperature; 3, replace the large pressure die casting machine. 4, add enough liquid metal, reduce the injection speed, increase the thickness of the feed port.